Choosing China’s top Metal Irregular Nozzle manufacturers requires more than comparing product photos. These components often serve custom spraying, cooling, mixing, or dosing systems. Their unusual geometry can affect flow direction, pressure loss, sealing, and maintenance. A reliable manufacturer should explain material selection, machining limits, surface finish, and application suitability. Stainless steel, brass, aluminum, and engineered alloys may perform differently in heat, corrosion, and abrasive environments. Small details matter. Thread accuracy matters. So does repeatability between batches.
This guide examines manufacturers through practical evidence, not marketing language. It considers engineering experience, drawing review, prototype support, inspection records, and communication during production. Useful checks include dimensional reports, flow testing, pressure testing where appropriate, and traceable material documentation. ISO certifications can support confidence, but they should not replace factory verification. A polished website is not proof. Samples may look excellent while production consistency remains uncertain. That is where buyers need careful questions and realistic expectations. No supplier is perfect. Even experienced teams can miss a tolerance or misunderstand an installation angle. Clear drawings, approved samples, and written acceptance criteria reduce that risk. The strongest candidates usually show stable processes, responsive technical support, and transparent limits. This comparison aims to help engineers and purchasing teams identify capable Chinese suppliers for dependable metal irregular nozzles, while recognizing that final selection must match actual working conditions.
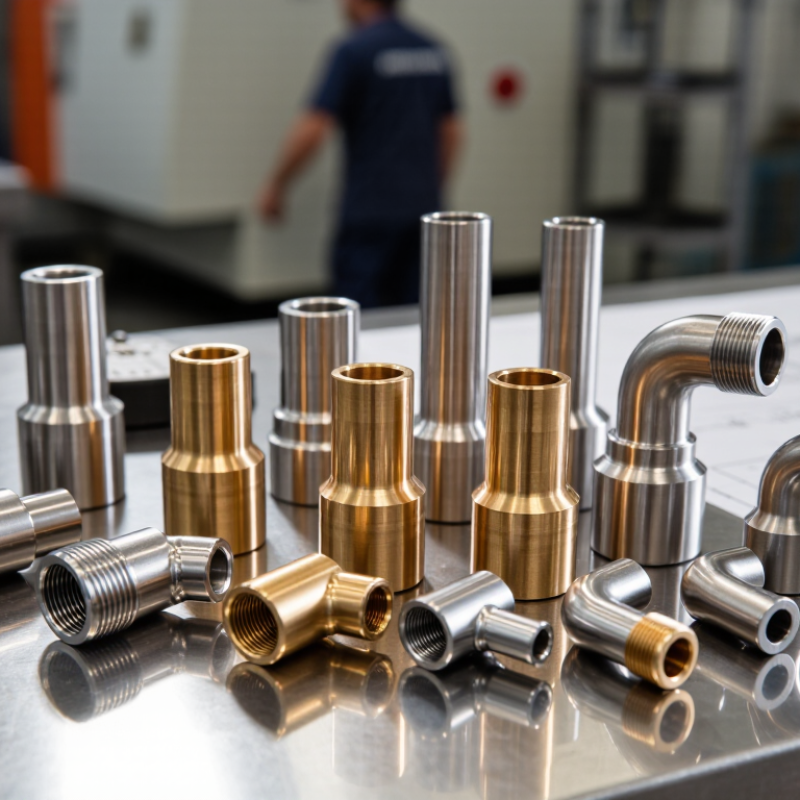
Metal irregular nozzles are engineered outlets with non-circular openings or uneven internal channels. Common designs include fan, slot, annular, multi-port, and elliptical patterns. Stainless steel, nickel alloys, brass, and titanium are selected according to temperature, corrosion, and pressure. The geometry controls spray angle, droplet size, impact force, and coverage. The term is not perfectly standardized. That gap matters.
These nozzles appear in spray drying, industrial washing, surface coating, combustion systems, food processing, and water treatment. A slot nozzle can create a wide, thin curtain across moving sheets. A multi-port nozzle can distribute cleaning fluid around complex equipment.
Grand View Research valued the global spray drying equipment market at roughly USD 5 billion in 2023 showing why precise atomization remains commercially important. Yet this figure covers equipment, not irregular nozzles alone.
China-based manufacturers commonly produce these parts through CNC machining, EDM, laser welding, and metal additive manufacturing. The Wohlers Report 2024 estimated the additive manufacturing industry reached USD 20.035 billion in 2023, supporting more complex flow-channel designs.
Reliable suppliers should provide material certificates, dimensional inspection, pressure testing, and measured flow-rate data. Engineers should also request spray-pattern tests at actual operating pressure. A drawing alone is insufficient.
In practice, I would question any supplier promising perfect uniformity without test conditions, because viscosity, temperature, and installation angle can change performance.
China’s irregular metal nozzles are usually made through a controlled, multi-stage process. Geometry changes everything. Engineers first convert the customer’s 3D model into machining paths and welding instructions. Common materials include stainless steel, carbon steel, and nickel-based alloys. China produced 1,005.1 million tonnes of crude steel in 2024, according to the World Steel Association. This supports strong material availability, but it does not guarantee consistent nozzle quality.
Manufacturers normally cut, forge, turn, mill, and weld the component according to its shape. Complex outlets may require five-axis machining to control wall thickness and internal flow. Automated production is expanding quickly. The International Federation of Robotics reported 276,288 industrial robot installations in China during 2023, representing 51% of global installations. Inspection still matters. Technicians check heat numbers, dimensions, weld appearance, surface finish, and pressure performance. A perfect drawing can still produce a poor part. Tool wear, distortion, and uneven polishing remain practical risks.
Tips: Request a material certificate, 3D drawing, tolerance table, weld procedure, and inspection plan. Ask for dimensional records and a flow or pressure test when performance is critical. Do not skip it. Some suppliers rely too heavily on visual inspection, especially around hidden internal passages. A sample nozzle should be reviewed before approving larger production.
| Manufacturing Dimension | Common Practice for Irregular Metal Nozzles | Typical Technical Data or Inspection Point | Application and Quality Significance |
|---|---|---|---|
| Engineering Input | Manufacturing normally begins with a 2D drawing, 3D CAD model, material specification, flow requirement, and connection details. | Key inputs include inlet and outlet dimensions, wall thickness, centerline offsets, pressure, temperature, medium, and surface-finish requirements. | Complete design data reduces rework and ensures that the irregular outlet geometry fits the assembly and delivers the required flow pattern. |
| Material Selection | Frequently used materials include stainless steel, carbon steel, aluminum, brass, and nickel-based alloys, selected according to the operating environment. | Common stainless-steel choices include 304/304L and 316/316L. Material certificates may verify chemical composition and mechanical properties. | 316/316L is generally preferred over 304/304L for chloride-containing or more corrosive service, while carbon steel is often used for lower-cost non-corrosive systems with suitable protection. |
| Blank Preparation | The initial blank may be produced from seamless or welded tube, plate, bar stock, forging, or a cast preform, depending on the nozzle shape and production quantity. | Blank dimensions are selected to provide machining allowance for the outer profile, internal passage, flange, and irregular outlet. | A correctly selected blank helps prevent distortion, excessive material waste, and insufficient wall thickness after machining. |
| CNC Turning | CNC turning is used for round inlet sections, cylindrical bodies, threads, shoulders, grooves, and sealing surfaces. | The process can control concentric features and repeatable diameters; final tolerance depends on material, geometry, machine capability, and drawing requirements. | Accurate inlet and sealing dimensions are important for assembly compatibility and leak prevention. |
| CNC Milling and 5-Axis Machining | Multi-axis milling is commonly used for non-round outlets, angled passages, compound surfaces, mounting faces, and asymmetric external profiles. | 5-axis machining can reduce repositioning and help maintain the relationship between the inlet axis, outlet axis, and internal flow passage. | This method is suitable for complex geometries that cannot be produced efficiently by standard two-axis turning alone. |
| Fabrication and Welding | For larger or highly customized nozzles, separate tube, plate, flange, and outlet components may be fitted and welded before finish machining. | Typical controls include qualified welding procedures, compatible filler metal, joint preparation, interpass temperature control, and weld inspection. | Welding can reduce material waste and enable large dimensions, but heat input and distortion must be controlled carefully. |
| Internal Passage Formation | Internal passages may be drilled, bored, milled, trepanned, or produced through a welded and machined construction. | Inspection focuses on bore diameter, transition radii, wall thickness, burr removal, and the absence of chips or obstructions. | Smooth transitions and clean passages help reduce turbulence, pressure loss, particle accumulation, and uneven discharge. |
| Thread, Flange, or Weld-End Connection | Connection ends may be threaded, flanged, socket-welded, butt-welded, or designed with a custom clamp or sanitary connection. | Verification may include thread gauge checks, flange dimensions, bolt-hole position, weld bevel angle, face flatness, and alignment. | Connection accuracy determines installation time, sealing performance, interchangeability, and maintenance convenience. |
| Heat Treatment | Heat treatment is selected according to the alloy, manufacturing route, service conditions, and required mechanical properties. | Possible controls include solution treatment for suitable stainless-steel grades, stress relief where applicable, and hardness verification. | Proper thermal processing can reduce residual stress and support corrosion resistance or dimensional stability, depending on the material. |
| Deburring and Edge Control | Machined edges are manually or mechanically deburred, with special attention given to internal intersections and outlet openings. | Checks include removal of sharp burrs, chips, loose particles, and excessive edge break that could affect flow or sealing. | Clean and controlled edges reduce contamination risks and protect gaskets, seals, operators, and downstream equipment. |
| Surface Finishing | Available finishes may include machining finish, grinding, polishing, bead blasting, pickling and passivation for suitable stainless-steel parts, or protective coating for carbon steel. | Surface roughness is specified by the drawing or application; internal surfaces may require a smoother finish than non-functional external areas. | Finishing influences corrosion resistance, cleanability, friction, appearance, and the behavior of the discharged medium. |
| Dimensional Inspection | Inspection may use calipers, micrometers, height gauges, thread gauges, bore gauges, optical equipment, and coordinate measuring machines. | Typical inspection points include overall dimensions, outlet profile, wall thickness, hole location, angularity, concentricity, and datum alignment. | Measurement against the approved drawing confirms that the irregular nozzle can be installed and operated as designed. |
| Non-Destructive Testing | Depending on risk and specification, manufacturers may use visual inspection, dye penetrant testing, magnetic particle testing, ultrasonic testing, or radiographic testing. | Dye penetrant testing is suitable for detecting surface-breaking discontinuities in many non-porous materials; ultrasonic and radiographic methods can examine weld or material integrity under appropriate conditions. | The selected method should match the material, joint type, thickness, acceptance criteria, and service risk. |
| Pressure and Leak Testing | Where required, completed nozzles or assemblies are subjected to hydrostatic, pneumatic, or low-pressure leak testing according to the approved procedure. | Test pressure, holding time, test medium, and acceptance criteria must be defined by the design code, purchase specification, or system requirement. | Testing verifies pressure containment and identifies leakage through welds, threaded areas, seals, or material defects. |
| Flow Verification | Flow testing is normally performed when the nozzle has a critical spray pattern, discharge angle, pressure drop, or distribution requirement. | Evaluation may include flow rate, pressure loss, discharge direction, spray coverage, velocity distribution, or particle size where relevant. | Dimensional conformity alone may not guarantee hydraulic performance for a complex irregular passage. |
| Documentation and Traceability | A controlled production file may include the approved drawing, material certificate, inspection report, weld records, surface-treatment record, and test results. | Traceability can be maintained through heat numbers, batch records, serial numbers, inspection status, and revision-controlled documents. | Clear documentation supports incoming inspection, regulatory compliance, maintenance, and repeat-order consistency. |
| Typical End-Use Sectors | Irregular metal nozzles are used in process piping, chemical equipment, water treatment, food and beverage systems, combustion equipment, dust-control systems, and industrial cooling or cleaning systems. | The required material, finish, testing, and connection design depend on the fluid, pressure, temperature, hygiene level, corrosion exposure, and installation method. | Application-specific engineering is essential because an appropriate nozzle design for one service may be unsuitable for another. |
Note: Technical values and inspection requirements for a specific irregular nozzle should be confirmed against its approved drawing, material standard, pressure class, applicable design code, and end-use conditions.
China Top Metal Irregular Nozzle Manufacturers?
High-quality metal nozzles begin with traceable materials, not appearance. ASTM material specifications should match pressure, temperature, corrosion, and welding conditions. Dimensional checks should cover bore diameter, wall thickness, angle, concentricity, and flange alignment. ISO 9001 controls help maintain these records, but certification alone proves little. The ISO Survey 2023 reported more than 1.26 million ISO 9001 certificates worldwide. That number shows broad adoption, not automatic product quality.
Pressure performance needs stronger evidence. Manufacturers should provide hydrostatic or pneumatic test records, weld inspection results, and heat-number traceability. ASME pressure-vessel and piping requirements may apply, depending on the nozzle’s final installation. Surface roughness also matters. A rough internal bore can increase turbulence, residue retention, and cleaning difficulty. Small defects become serious at high flow rates. They may not appear during visual inspection.
Industry data supports this caution. The International Energy Agency’s Energy Technology Perspectives 2024 highlights rising pressure on industrial equipment to improve efficiency and reduce material waste. For irregular nozzles, accurate geometry supports both goals. However, a perfect drawing cannot replace testing. This is where procurement teams sometimes overestimate paperwork. A certificate may be genuine, yet the inspection scope can remain too narrow. High-quality suppliers should welcome dimensional reports, material certificates, non-destructive testing, and sample verification before shipment. The standard is evidence, not confidence.
This chart shows the general linear dimensional tolerances for tolerance class “m” in ISO 2768-1. These values can be used as a basic benchmark when reviewing machined metal nozzle dimensions. High-quality irregular nozzles should also be evaluated against the technical drawing, applicable material standard, surface-finish requirements, geometric tolerances, and pressure or leakage-test specifications.
Reference: ISO 2768-1, General tolerances for linear and angular dimensions, tolerance class m. The applicable product specification takes precedence over general tolerances.
Evaluating China’s leading irregular nozzle manufacturers requires more than comparing prices. Start with engineering capability. Request material certificates, dimensional reports, welding procedures, and pressure-test records. Review how the factory converts complex drawings into stable production. Ask about tolerances around openings, flange alignment, wall thickness, and surface treatment. A reliable manufacturer should explain these details clearly, not hide behind general claims. Samples should match the approved drawing and remain consistent across repeated batches.
Factory experience also matters. Examine similar projects, available machining equipment, inspection tools, and the qualifications of quality personnel. A video tour helps, but an independent audit offers stronger evidence. Check whether the supplier controls raw materials from receipt to shipment. Communication is another practical test. Send one detailed drawing and observe the response. Vague answers may signal weak technical support. No supplier is perfect. A small documentation gap can be corrected, but repeated measurement errors deserve caution.
Tips: Compare at least three factories using the same specification sheet. Ask for a first-article inspection before full production. Confirm packaging for sharp edges, moisture, and deformation. Keep every revision in writing. Do not select the lowest quotation automatically; an inexpensive nozzle can create costly installation delays. I would also inspect rejected parts during a factory visit, because they reveal more than polished samples.
Pricing begins with the alloy, geometry, and production volume. Stainless steel, nickel alloys, and titanium behave differently during machining and forming. Complex angles can require five-axis machining, special fixtures, or secondary polishing. Grand View Research’s 2024 metal fabrication analysis forecasts steady market growth through 2030, but energy, labor, and equipment costs still vary by region. A low quotation can be a warning, not a victory.
Customization affects both cost and risk. Engineers should specify flow rate, pressure, temperature, connection size, surface roughness, and allowable tolerance. A nozzle with a 0.05 mm opening tolerance needs stricter inspection than a general-purpose part. Material certificates, dimensional reports, and pressure-test records add expense, yet they protect production reliability. ISO 9001 registration supports process control, but it does not prove every nozzle meets the drawing. I would request samples.
Delivery depends on more than machining time. Raw-material availability, drawing approval, tooling, inspection queues, and export scheduling can each add days. The World Bank’s Commodity Markets Outlook, October 2024, projected a 5% decline in broad commodity prices for 2025, but price movements remain uneven across industrial metals. Buyers should lock the quotation period and identify adjustment rules. Deloitte’s 2024 Global Chief Procurement Officer Survey also highlights supply continuity as a major procurement concern. In practice, a realistic delivery window beats an attractive promise.